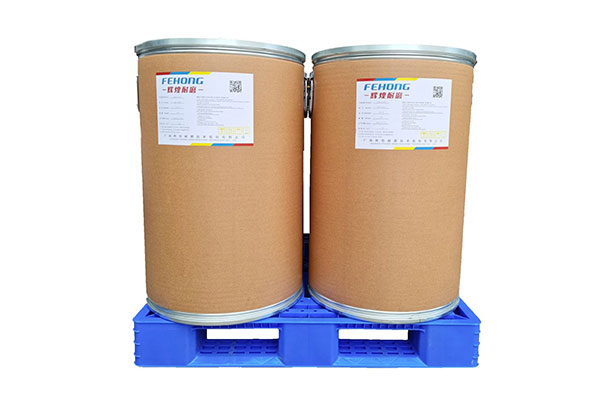
FCW Wire For Cement Plant Header
HH-806 Hardfacing flux cored welding wire

HH-806 Hardfacing flux cored welding wire

Model Number: HH-806
Hardness: 200 - 250 HB
Chemical Composition (C): 0.08 - 0.15%
Chemical Composition (Cr): 10.0 - 13.0%
Chemical Composition (Mn): 13.0 - 16.0%
Chemical Composition (Si): 0.4 - 0.8%
Chemical Composition (Ni): 0.2 - 0.5%
Chemical Composition (V, Ti, Mo + Others): Suitable amount
Welding Current: 350 - 430 A
Welding Voltage: 27 - 32 V
Microstructure: Austenitic manganese steel (C - Cr - Mn - Fe)
Packaging: 250 kg/drum; 125 kg/drum
More Details

HH-806 Hardfacing flux cored welding wire

Welding the buffer layer (build-up layer) of the grinding rollers (VRM) & press roller (HPGR)

Characteristics

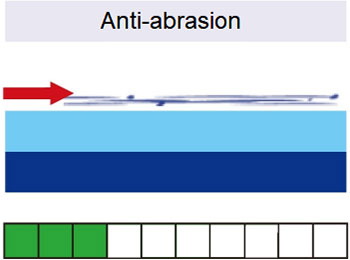
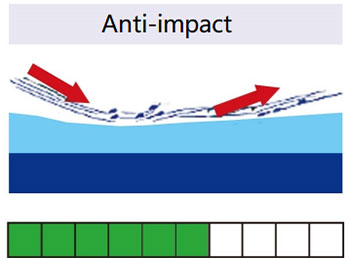
HH-806 produces an austenitic (non-magnetic) tough and crack-free weld deposit. Shock impact result in superficial work-hardening. The weld deposit is characterized by its good compatibility with all weldable steels. The hardfacing material is not suited for flame-cutting.

1. Microstructure: Manganese steel, austenitic on iron base with chromium: C – Cr – Mn – Fe.
2. Machinability: Grinding only.
3. Cutting: Not suited for flame-cutting.
4. Deposit thickness: Multi layers.

Specification

DIN EN 14700 T Fe9 kp

Application

Perfectly suited for tough and pressure-resistant buffer layers and for the hardfacing of parts which are mainly subjected to impact, e.g. Mill Roller, Mill Table, Press Roller, Rotor of Crusher.

Typical compositions of pure welded deposit

C Cr Si Ni Mn V, Ti, Mo, others
0.08-0.15% 10.0-13.0% 0.4-0.8% 0.20-0.50% 13.0-16.0% suitable

Hardness of pure welded deposit

200-250 HB

Package

250 KG / drum, 125 KG / drum

Recommended welding parameters

Φ Amperage [A] Voltage [V] Wire stick-out [MM]
2.8 mm 350-430 27-32 25~40

Welding Precautions

  1. When using HH-806 welding wire, do not use inert gas. During welding, carefully control the current and voltage according to the recommended surfacing parameters.
  2. Both weaving and straight bead are possible. Multiple layers can be welded. The performance of the surfacing alloy layer is related to the surfacing dilution rate and bead form.
  3. After each weld layer is completed, the weld slag must be cleaned before welding the next layer, and so on.
HH-806 HH-806 HH-806 HH-806

Note: This data sheet corresponds to the present state of production (August 2026) and can be changed anytime.

Get in Touch

Have questions or want to discuss a project? We're here to help. Fill out the form and our team will get back to you as soon as possible.