FCW Wire For Cement Plant Header
HH-810 Hardfacing flux cored welding wire

HH-810 Hardfacing flux cored welding wire

Model Number: HH-810
Hardness: ≥ 60 HRC
Chemical Composition (C): 4.5 - 6.0%
Chemical Composition (Cr): 25 - 32%
Chemical Composition (Mn): 0.5 - 1.0%
Chemical Composition (Si): 0.7 - 1.5%
Chemical Composition (Mo): 1.0 - 2.0%
Chemical Composition (Ni, V, Ti, Nb + Others): suitable
Welding Current: 360 - 430 A
Welding Voltage: 28 - 32 V
Max Operating Temperature: ≤ 500°C
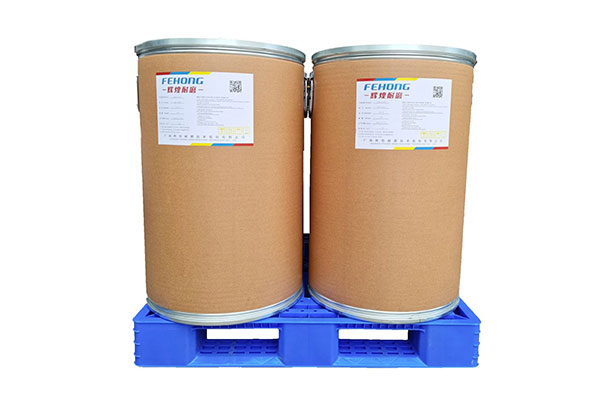
Packaging: 250 kg/drum; 125 kg/drum
More Details

HH-810 Hardfacing flux cored welding wire

Welding the hardfaced layer (build-up layer) of the grinding rollers (VRM) & press roller (HPGR)

Characteristics

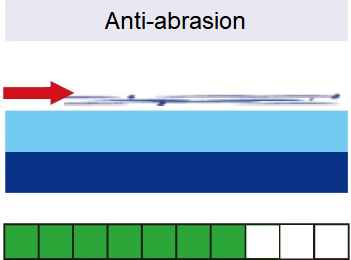
HH-810 produces a wear-resistant, austenitic, primary carbide-containing weld deposit. It is very resistant to abrasion.

1. Microstructure: High-chrome-high-carbon hard alloy on iron base with molybdenum additions, C – Cr – Mo – Fe.
2. Machinability: Grinding only.
3. Cutting: Not suited for flame-cutting.
4. Deposit thickness: Multi layers.

Specification

EN14700 T Z FE 15g

Application

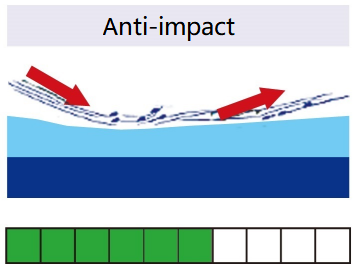
Recommended particularly for the hardfacing of parts subjected to strong abrasion and medium impact stress, e.g. Vertical mill rollers, Mill discs, Roll presses, Sieves, Stirrer blades, Sand slingers and Top coats of Dredger teeth. The application temperatures should not exceed 500℃.

Typical compositions of pure welded deposit

C Cr Si Mn Mo Ni, V, Ti, Nb, others
4.5-6.0% 25-32% 0.7-1.5% 0.5-1.0% 1.0-2.0% suitable

Hardness of pure welded deposit

≥ 60 HRC

Package

250 KG / drum, 125 KG / drum

Recommended welding parameters

Φ Amperage [A] Voltage [V] Wire stick-out [MM]
2.8 mm 360-430 28-32 25~40

Welding Precautions

  1. When using HH-810 welding wire, do not use inert gas. During welding, carefully control the current and voltage according to the recommended surfacing parameters.
  2. Both weaving and straight bead are possible. Multiple layers can be welded. The performance of the surfacing alloy layer is related to the surfacing dilution rate.
  3. After each weld layer is completed, the weld slag must be cleaned before welding the next layer, and so on.
HH-810 HH-810 HH-810 HH-810

Note: This data sheet corresponds to the present state of production (August 2026) and can be changed anytime.

Get in Touch

Have questions or want to discuss a project? We're here to help. Fill out the form and our team will get back to you as soon as possible.